Industrial NIR Analyzer
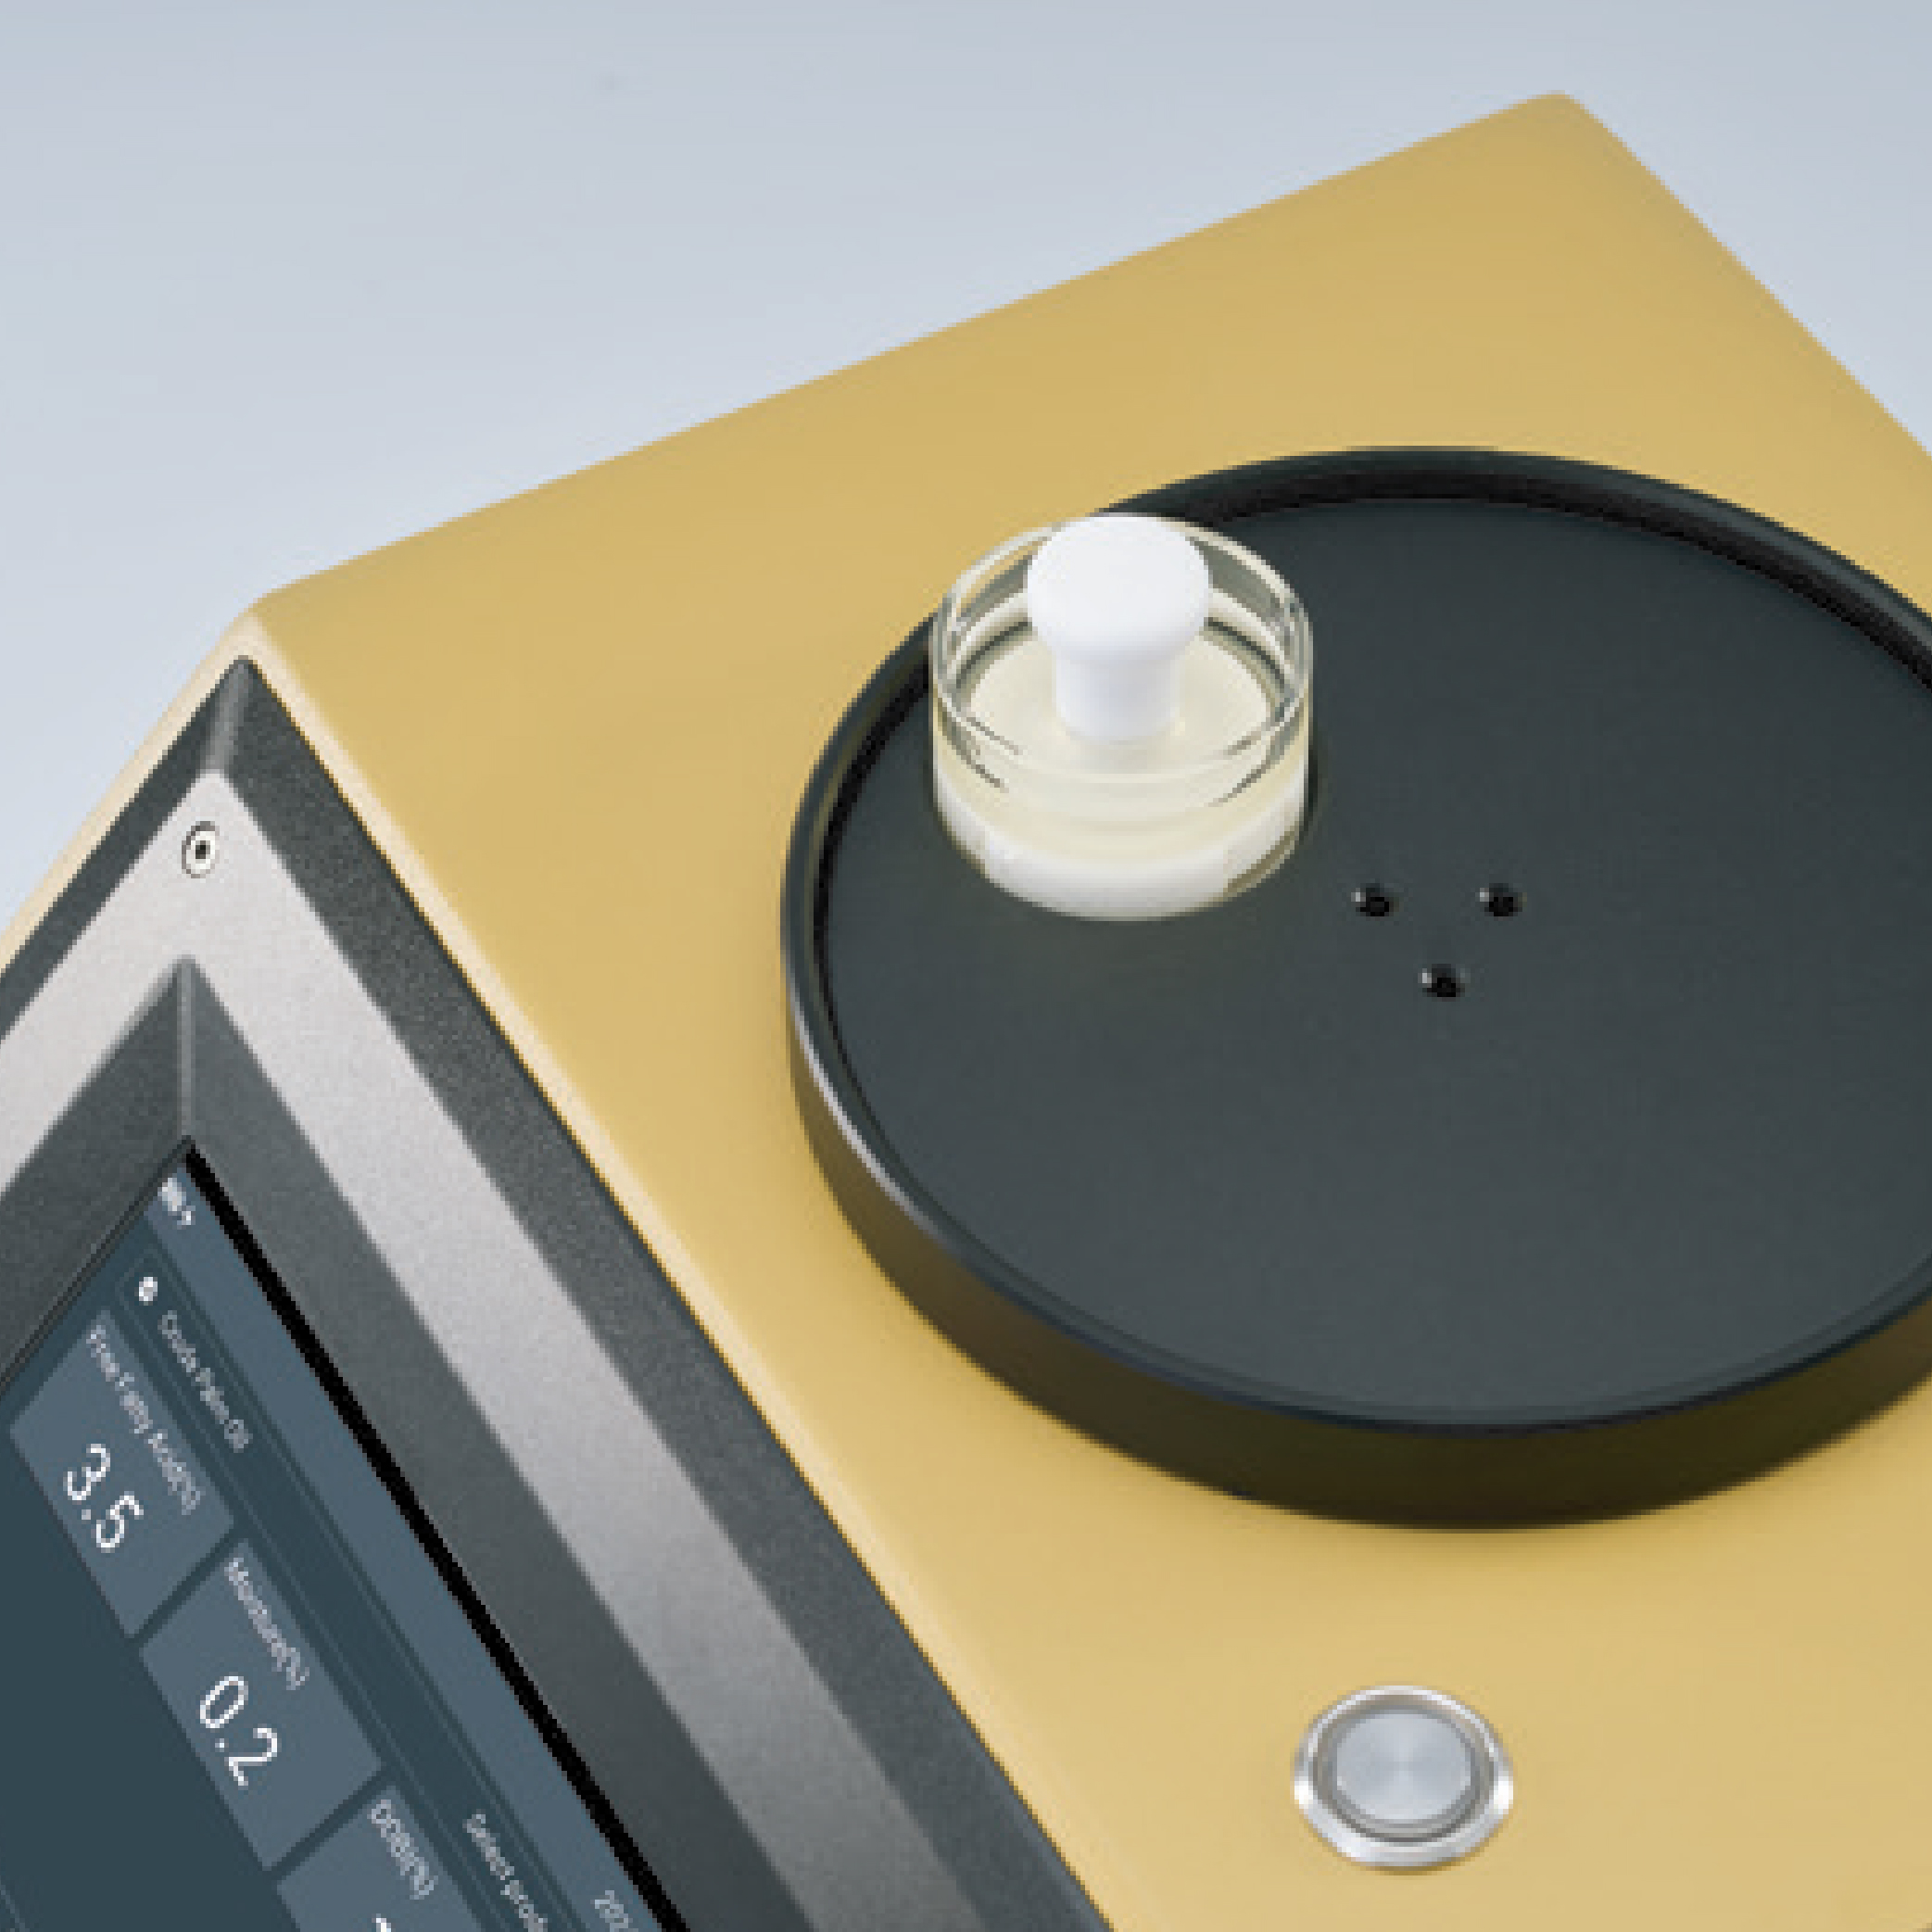
Advanced Industrial NIR Analyzer for Fast and Reliable Material Analysis
Benchmarck Scientific provides laboratory and industrial analytical equipment solutions, including Industrial NIR Analyzer options for manufacturing, processing, research, and quality control applications.
An Industrial Near-Infrared (NIR) Analyzer is an analytical instrument that uses near-infrared spectroscopy to evaluate selected material properties rapidly. Depending on the instrument configuration and calibration model, it can help monitor parameters such as moisture, protein, fat, oil, and other quality characteristics.
Industrial NIR analyzers can support routine testing, production monitoring, and process optimization across various industries. They are suitable for applications where rapid analytical information can help improve operational efficiency and product consistency.
What Is an Industrial NIR Analyzer?
An Industrial NIR Analyzer is designed to analyze materials in industrial environments using near-infrared light. The instrument measures the spectral response of a sample, and appropriate calibration models are used to estimate specific chemical or physical properties.
Depending on the application, an industrial NIR system may be configured for at-line, online, or in-line analysis. These configurations can help manufacturers monitor material quality during different stages of production and processing.
Industrial NIR analyzers are used in food processing, agriculture, animal feed production, chemical manufacturing, and other industries that require efficient material analysis.
Key Features of Industrial NIR Analyzer
1. Rapid Material Analysis
Obtain analytical results quickly for supported samples and measurement parameters, helping reduce delays in routine quality control.
2. Multi-Parameter Measurement
Suitable systems can estimate multiple material properties using validated calibration models for the specific application.
3. Industrial Process Monitoring
Selected configurations can support at-line, online, or in-line measurement to help monitor material quality during production.
4. Reduced Sample Preparation
For suitable applications, NIR analysis can reduce the need for extensive sample preparation and chemical reagents.
5. Quality Control Support
Help identify variations in raw materials, intermediate products, and finished products through routine measurements.
6. Data Recording and Reporting
Depending on the instrument software, users can record analytical results, generate reports, and review measurement trends.
7. Flexible Application Options
Industrial NIR systems may be available in different configurations to suit laboratory, production-line, and process-monitoring requirements.
Applications of Industrial NIR Analyzer
Food Processing Industry
Industrial NIR analyzers can support the evaluation of moisture, protein, fat, and other relevant parameters in suitable food ingredients and processed products.
Agriculture and Grain Processing
Used for the analysis of grains, cereals, oilseeds, and other agricultural materials with appropriate calibration models.
Animal Feed Manufacturing
Can help estimate selected nutritional parameters in raw materials, feed mixtures, and finished feed products.
Oilseed and Edible Oil Industry
Suitable systems may be configured to evaluate selected quality parameters in oilseeds and edible oil-related materials.
Chemical Manufacturing
Can support the monitoring of selected material properties and process conditions in compatible chemical applications.
Pharmaceutical Manufacturing
NIR spectroscopy can support raw material identification, blend assessment, and selected process analytical applications when properly validated.
Industrial Research and Development
Useful for material characterization, method development, process studies, and quality assessment in research environments.
Benefits of Industrial NIR Analyzer
- Faster routine material analysis.
- Improved efficiency in quality control workflows.
- Potential reduction in chemical reagent consumption for suitable applications.
- Support for monitoring raw materials and finished products.
- Improved visibility into material variations during production.
- Potential reduction in routine testing time and operating costs.
- Support for data-driven process optimization.
Actual benefits depend on the application, instrument configuration, calibration performance, and operating conditions.